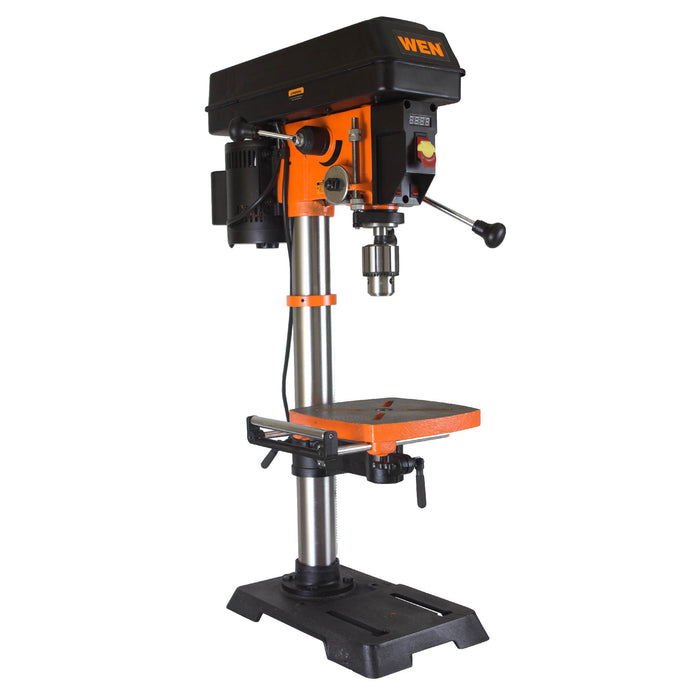
A drilling station for repeated parts
4214T can make sense when a joiner repeatedly drills supported components and wants a fixed spindle approach with a depth stop. It is a benchtop machine, so the purchase still needs a stable mounted position and appropriate workholding. The 12-inch swing and stated travel describe limits; check the actual hole location and assembled stock height before assuming a compact machine covers the component.
Set speed for the accessory
WEN documents a mechanical speed range of 580 to 3,200 RPM and a digital readout. That makes the selected speed visible, but it does not choose the correct setting for a bit, diameter or material. The laser and light assist setup rather than proving hole accuracy. A supported fence or jig can help a repeat operation; do not treat a drill press as a milling machine or improvise unsupported sideways cutting.
Budget for the drilling arrangement
Include suitable bits, workholding and any purpose-built table needed for the actual stock. An occasional hole can often be covered by the drill already in the kit, while a batch of repeated components can justify a fixed station. Compare usable throat and travel instead of motor size alone. We have not measured spindle runout or repeatability; the recommendation concerns documented format and the operation it may organize.